ForceBeyond Logo
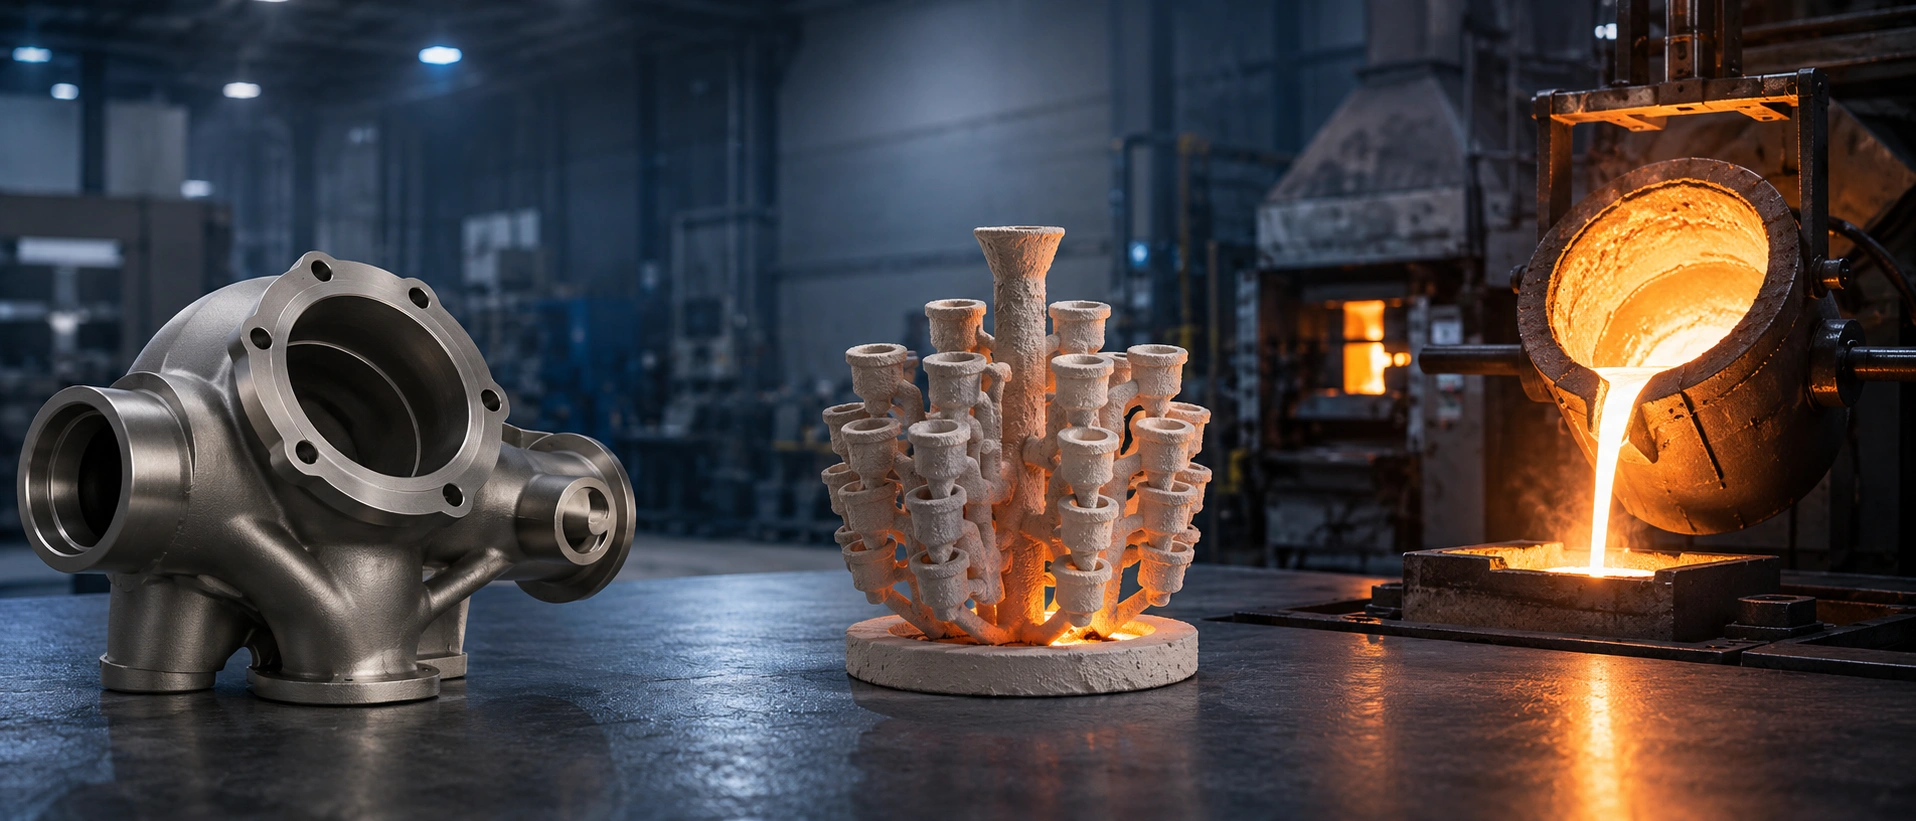
Investment casting process with wax patterns and ceramic shell preparation

Investment Casting Services: Precision Lost-Wax Metal Components

Custom Investment Casting for Complex Metal Components

Investment casting (lost-wax precision casting) is an engineered net-shape metal forming process manufactured using expendable wax patterns and ceramic refractory shells to produce complex aerospace, turbine, valve, pump, and industrial components with as-cast surface finishes down to 125 Ra (3.2 µm) and dimensional tolerances to ISO 8062-3 DCTG 4. ForceBeyond provides custom investment casting services for complex, near-net-shape metal components. Also known as the lost-wax process, investment casting uses a sacrificial pattern and ceramic shell to reproduce detailed geometry, thin sections, smooth surfaces, and features that may be difficult or uneconomical to machine from solid stock.

Programs may include stainless steel, carbon and low-alloy steel, nickel-based superalloys, and titanium investment casting. ForceBeyond coordinates casting, heat treatment, precision machining, HIP, surface finishing, inspection, assembly, and logistics through an integrated manufacturing network.

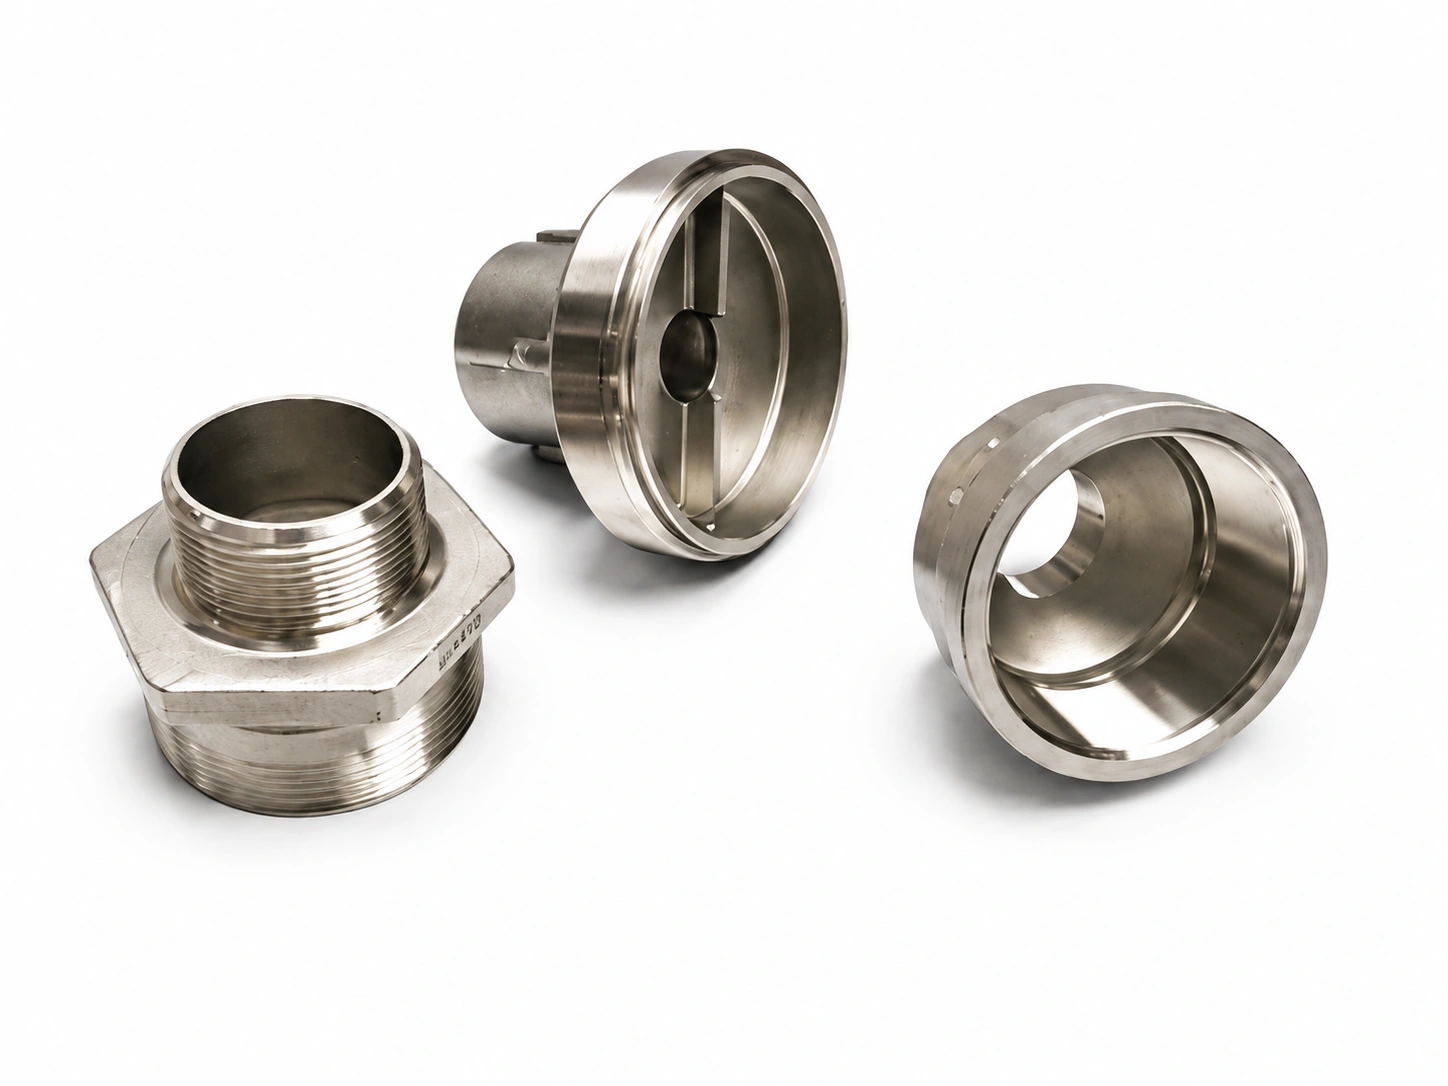
Precision investment-cast stainless steel valve and fitting components with machined threads and internal bores on a white background

When to Choose Investment Casting

Investment casting is often selected when part complexity, alloy cost, surface finish, dimensional control, and reduced machining are more important than the lowest possible tooling cost.

  • Complex geometry: contours, ribs, bosses, internal passages, fine details, and reduced draft requirements.
  • Thin or variable sections: designs requiring controlled wall transitions and geometry that would be difficult to form by sand casting.
  • High-cost alloys: near-net shapes can reduce material waste when using titanium, Inconel, and other expensive alloys.
  • Surface and appearance: smooth as-cast surfaces can reduce polishing, grinding, and machining requirements.
  • Consolidated parts: multiple machined or fabricated pieces may sometimes be redesigned as one casting.

Investment Casting vs. Sand Casting

The table below provides typical process guidelines. Final capability depends on alloy, geometry, part size, foundry process, tooling, production volume, and drawing requirements.

Selection Factor Investment Casting Sand Casting
Surface Finish Typically smoother; approximately 63–125 RMS may be achievable on suitable geometries. Typically rougher; often approximately 250–500 RMS depending on molding process and alloy.
Dimensional Control Typical linear tolerance may approach ±0.005 in/in, subject to geometry and foundry capability. Broader tolerances are common, especially on larger parts and complex mold joints.
Wall Thickness Small features may approach about 0.040 in (1.0 mm), subject to alloy and flow length. Generally requires thicker sections, especially on large or long-flow geometries.
Part Size and Tooling Best suited to small and medium complex components where precision offsets tooling cost. Often preferred for larger parts, simpler geometry, and lower tooling investment.

Investment Casting Materials and Alloy Capabilities

The investment casting process supports a broad range of ferrous and non-ferrous alloys. Material selection should consider mechanical properties, corrosion resistance, temperature, weldability, machinability, heat treatment, and applicable specifications.

Investment Casting Alloy Mechanical Specifications & Quality Standards
Material Category & Spec Representative Alloys Tensile Strength (UTS) Yield Strength (0.2%) Applicable Standard / Verification
Stainless Steel (ASTM A743) 316L, 17-4 PH, CF8M 75 – 150 ksi (517 – 1034 MPa) 30 – 115 ksi (207 – 793 MPa) ASTM E8 tensile, AMS 5355, ASTM E1417 (FPI)
Nickel Superalloys (AMS 5383) Inconel 718, Inconel 625 100 – 145 ksi (689 – 1000 MPa) 50 – 125 ksi (345 – 862 MPa) ASTM E21 elevated temp, AMS 5401, ASTM E1742
Titanium Alloys (ASTM B367) Ti-6Al-4V Grade C-5 130 – 145 ksi (896 – 1000 MPa) 120 – 135 ksi (827 – 931 MPa) AMS 4991, ASTM E8, AS9100D, ISO 9001:2015
Carbon & Low-Alloy (ASTM A216) WCB, 8620, 4140 70 – 105 ksi (483 – 724 MPa) 36 – 85 ksi (248 – 586 MPa) ASTM A148, ASTM E1444 (MPI) magnetic particle

Step-by-Step Lost-Wax Investment Casting Process

  1. Pattern production: wax or printed patterns reproduce the component geometry and are attached to a central runner system.
  2. Ceramic shell building: the pattern assembly is repeatedly dipped in refractory slurry and coated with ceramic stucco until the required shell thickness is achieved.
  3. Dewaxing and firing: wax is removed, and the ceramic shell is fired to develop strength and prepare it for pouring.
  4. Melting and pouring: the selected alloy is melted and poured into the heated shell. Vacuum processing may be used for reactive or high-performance alloys.
  5. Knockout and cutoff: after solidification, the shell is removed and individual castings are separated from the runner system.
  6. Finishing and inspection: gates are removed, surfaces are blended, and parts proceed through heat treatment, HIP, machining, coating, and inspection as required.

Investment Casting Design Guidelines

Early manufacturability review can reduce tooling changes, distortion, shrinkage risk, and unnecessary machining.

  • Wall transitions: avoid abrupt section changes that can create hot spots, shrinkage, or feeding problems.
  • Fillets and radii: use practical internal radii to improve shell strength, metal flow, and stress distribution.
  • Machining allowance: add controlled stock only where functional dimensions require final machining.
  • Datum strategy: establish repeatable locating surfaces for machining and inspection.
  • Parting and gating: review gate location, cutoff access, ceramic-shell support, and potential distortion before tooling release.

Prototype and Production Investment Casting

Prototype investment casting may use printed wax or SLA patterns to support design validation, low-volume production, and alloy testing before hard tooling is released. Production programs typically use dedicated wax-injection tooling for repeatability and cycle efficiency.

The best approach depends on annual volume, part size, pattern cost, inspection requirements, delivery timing, and expected design changes.

Investment Casting, Machining and Secondary Operations

Near-net investment casting can reduce material removal, but many functional parts still require coordinated secondary operations.

  • Precision CNC machining: milling, turning, drilling, tapping, and grinding for datums, bores, threads, sealing surfaces, and mating features.
  • Heat treatment: alloy-specific solution treatment, aging, stress relief, and mechanical-property development.
  • Hot Isostatic Pressing: density improvement for suitable alloys and defect types, coordinated with heat treatment and inspection.
  • Surface finishing: passivation, electropolishing, blasting, polishing, coating, and project-specific protective treatments.
  • Inspection and NDT: dimensional inspection, radiography, penetrant inspection, material verification, and documentation as required by the project.
  • Assembly and kitting: inserts, bearings, hardware, sub-assembly, labeling, and protective packaging.

Investment Casting Applications by Industry

Frequently Asked Questions: Investment Casting

How does investment casting compare with sand casting?

Investment casting generally provides finer surface finishes, tighter dimensional control, thinner walls, and greater geometric detail than sand casting. Sand casting is often more economical for larger parts, simpler shapes, and lower tooling budgets. Final process selection depends on alloy, geometry, part size, production volume, tolerance, surface finish, and cost targets.

What wall thickness can investment casting achieve?

Wall thickness depends on alloy fluidity, part size, flow length, geometry, local section transitions, and foundry process capability. Small features may approach approximately 0.040 in (1.0 mm), while more conservative designs often use 0.060 to 0.125 in or greater. Minimum wall thickness should be confirmed during manufacturability review.

Can ForceBeyond support prototype investment castings?

Yes. Prototype programs may use 3D-printed patterns, printed wax, or SLA patterns to produce ceramic shells without committing immediately to hard production tooling. This approach can support design validation, alloy testing, fit checks, and low-volume development before production tooling is released.

What information is needed for an investment casting quote?

Provide a 2D drawing and, when available, a 3D CAD model, along with material grade, annual and batch quantity, critical tolerances, wall-thickness requirements, surface finish, heat treatment, HIP, machining, inspection, certification, and delivery requirements. Clearly identify critical-to-quality features and any customer or industry specifications.

Request an Investment Casting Quote

Send your drawing, CAD model, material grade, quantity, tolerance, wall-thickness, machining, heat-treatment, inspection, and delivery requirements for an engineering review.

Technical References
Related Investment Casting, Machining, Quality and Materials Resources